
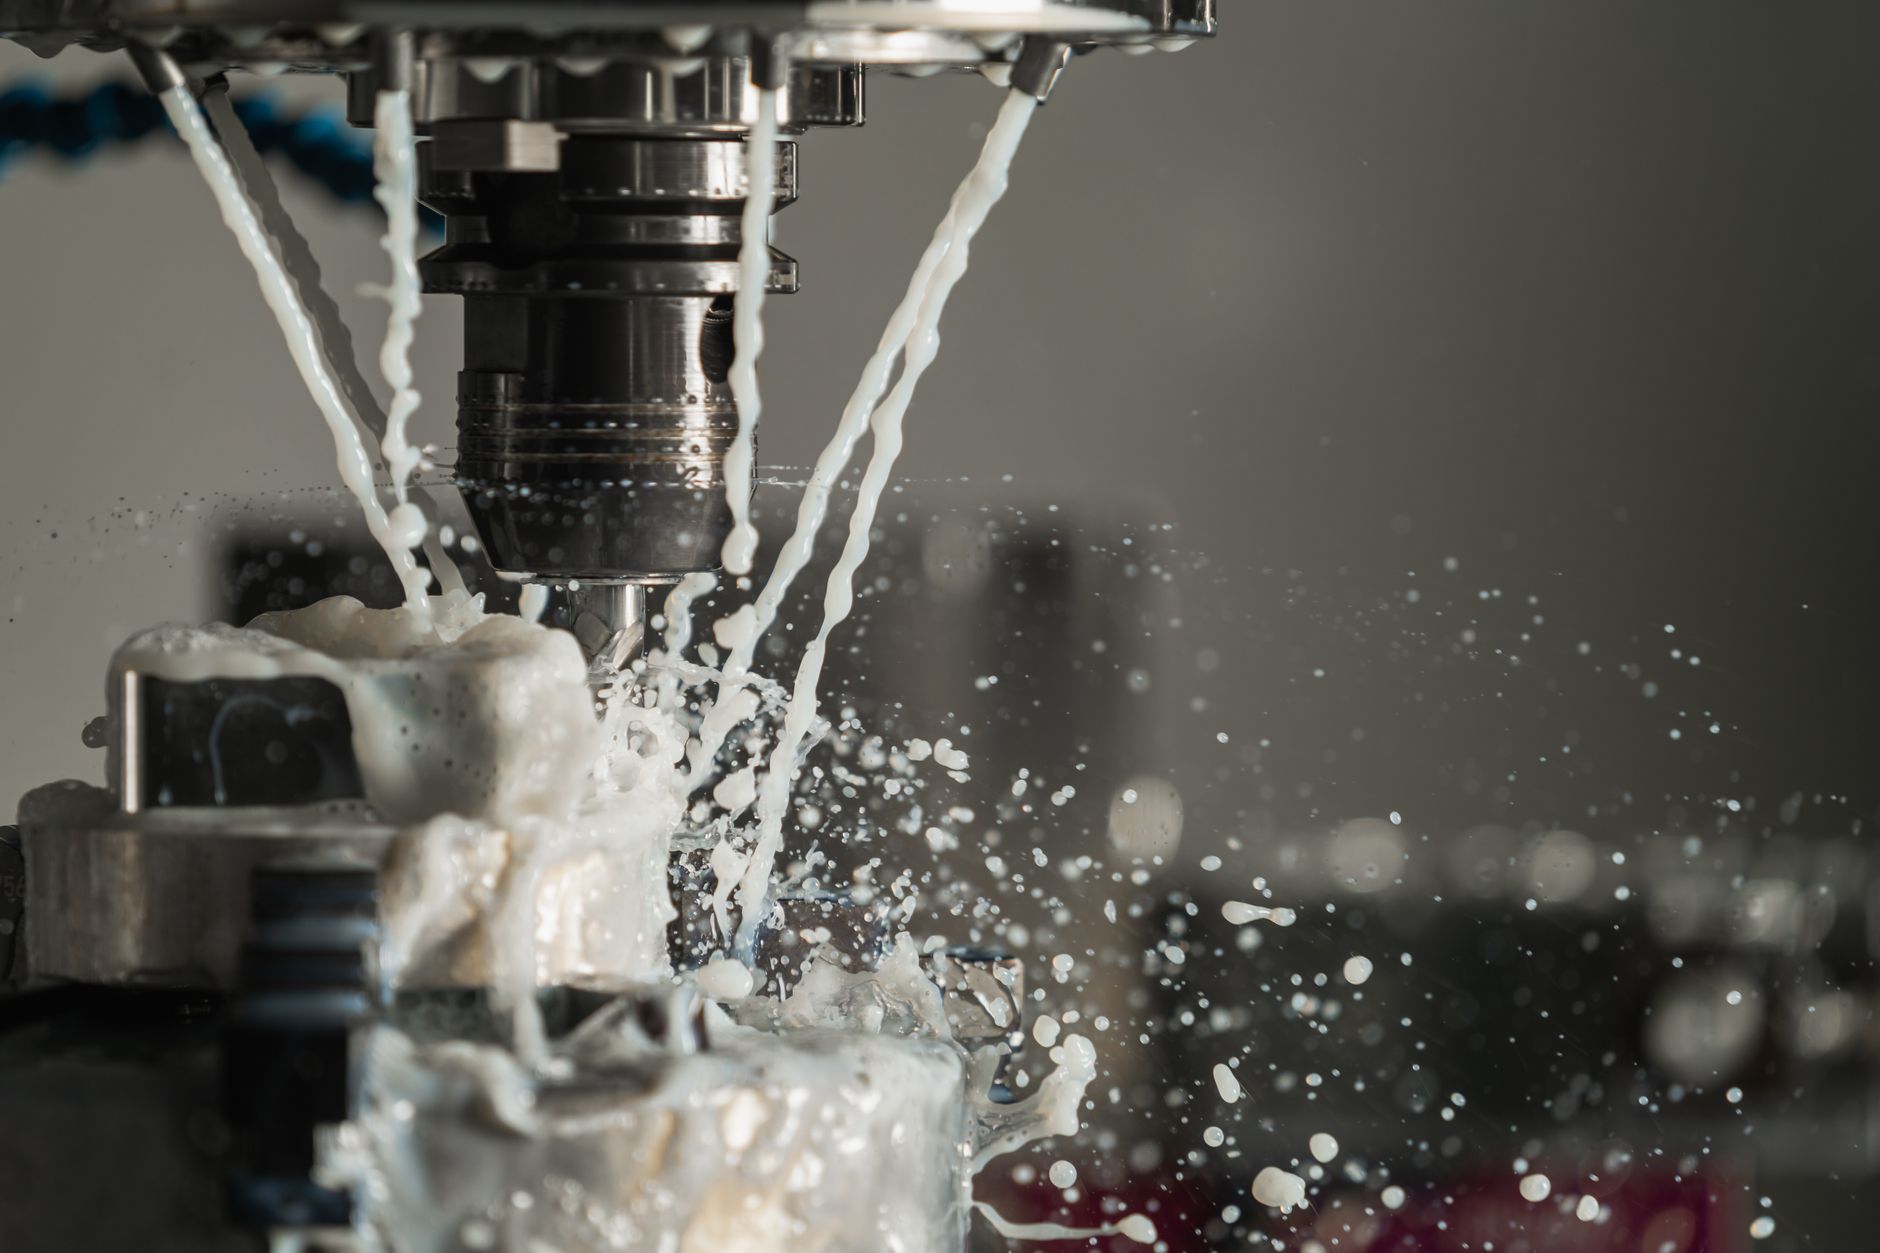
Mould design & DFM
Every enquiry starts with a design-for-manufacture review: gating and cooling laid out in Moldflow, tolerances agreed against your drawing, and a tooling plan costed before a single block is cut.
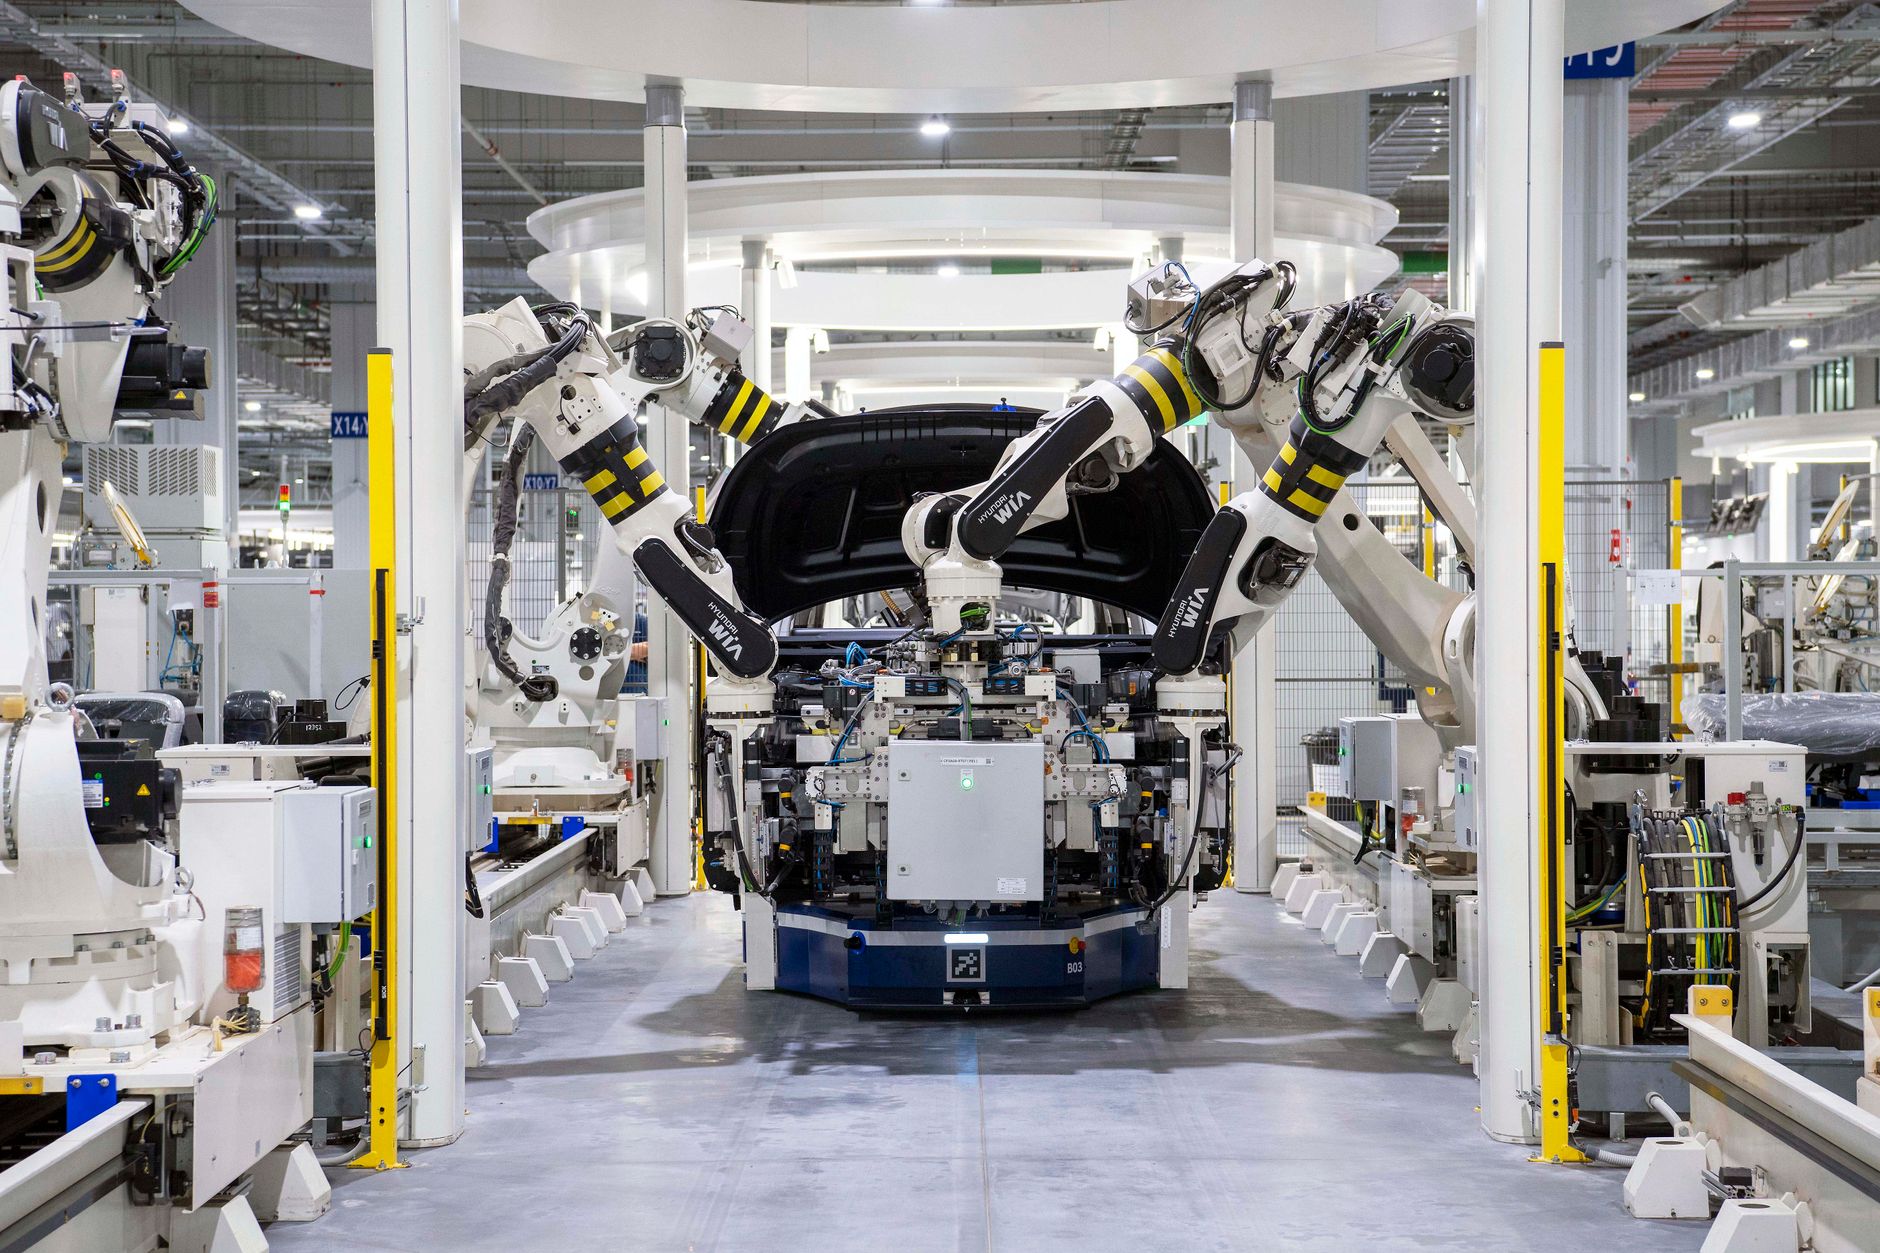
Contract toolmaking & injection moulding · Penang
Keystone Mould is a Tier-1 moulding partner for automotive, medical and electronics manufacturers across Malaysia — from DFM review and hardened tooling to validated, high-cavitation production.
Trusted on the line by manufacturers across Malaysia
What we run
Every enquiry starts with a design-for-manufacture review: gating and cooling laid out in Moldflow, tolerances agreed against your drawing, and a tooling plan costed before a single block is cut.
CNC milling, sinker & wire EDM, jig grinding and full spotting presses for tools up to 6 tonnes.
48 presses from 50 to 850 tonne, all with robots, gravimetric dosing and cavity-pressure monitoring.
Vertical and shuttle cells for brass inserts, stampings and two-shot soft-touch parts.
An ISO Class 8 (100,000) bay for medical and optical components, gowned and particle-counted.
Pad printing, ultrasonic welding, leak testing and kitted sub-assembly, done in-house.
Capacity, in plain numbers
Family-owned since 2003, Batu Kawan
50–850 tonne, all robot-served
Across 60+ active production tools
Verified on CMM and vision
ASEAN, EU, North America, Japan
From enquiry to first shipment
Send the drawing, resin and annual volume. We return a DFM note, a tooling quote and a lead time, usually within three working days.
The mould is cut and assembled in our tool room, then sampled. You get T1 parts with a full dimensional report.
Process windows are set and locked, capability is proven, and we submit ISIR or full PPAP to your requirement.
Scheduled runs with in-line checks, then kitted, labelled and shipped — ex-works, DAP or into your VMI bins.
Selected work
Under NDA we can name names; here is the shape of the work — the part, the sector, and what mattered about the tool.
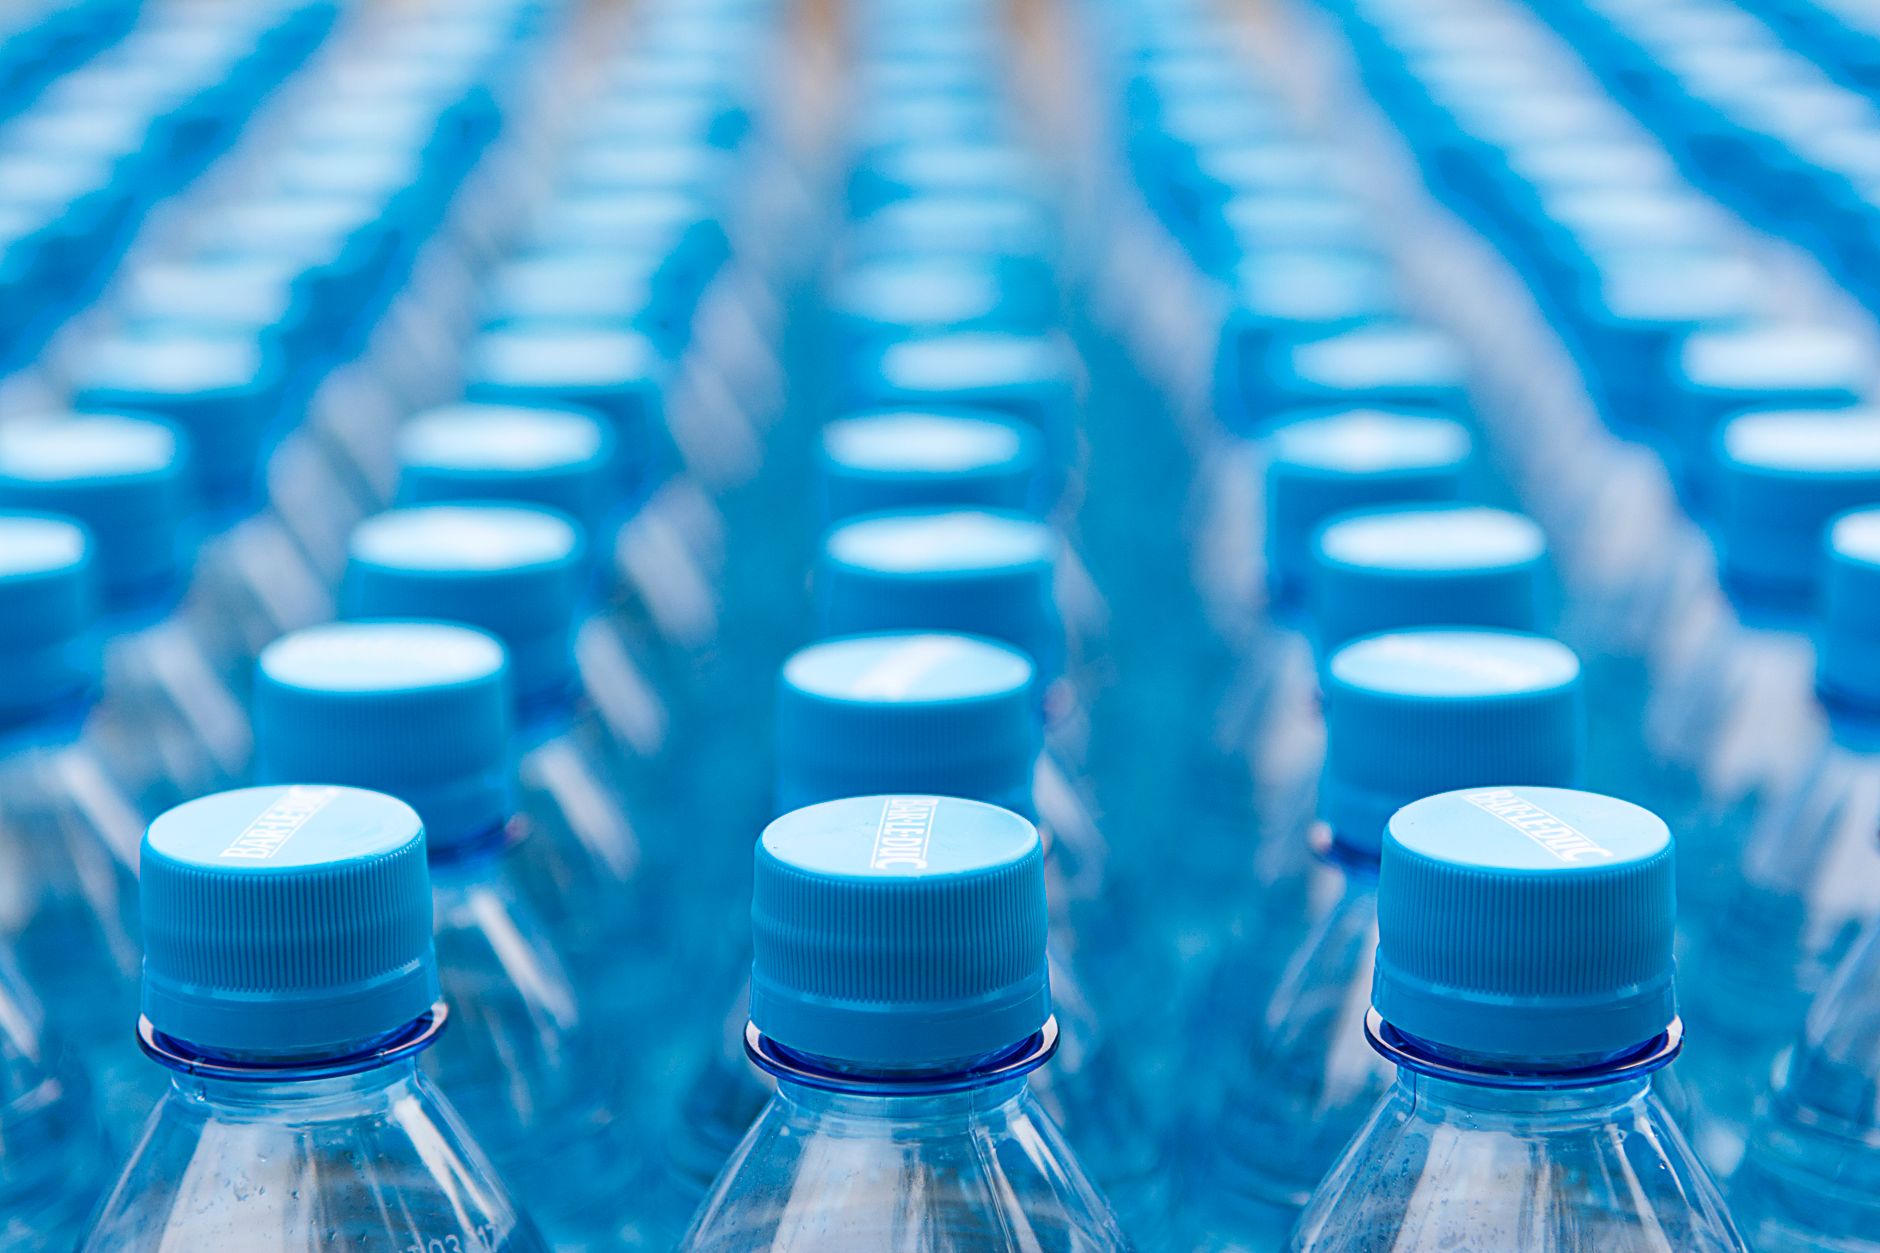
Beverage
A thin-wall PP closure for a regional bottler, moulded on a 250-tonne cell at a 4.1-second cycle. A hot-runner valve gate and conformal cooling hold the slip band flat across all sixteen cavities; we run 2.4 million a week to a VMI bin at their filling hall.
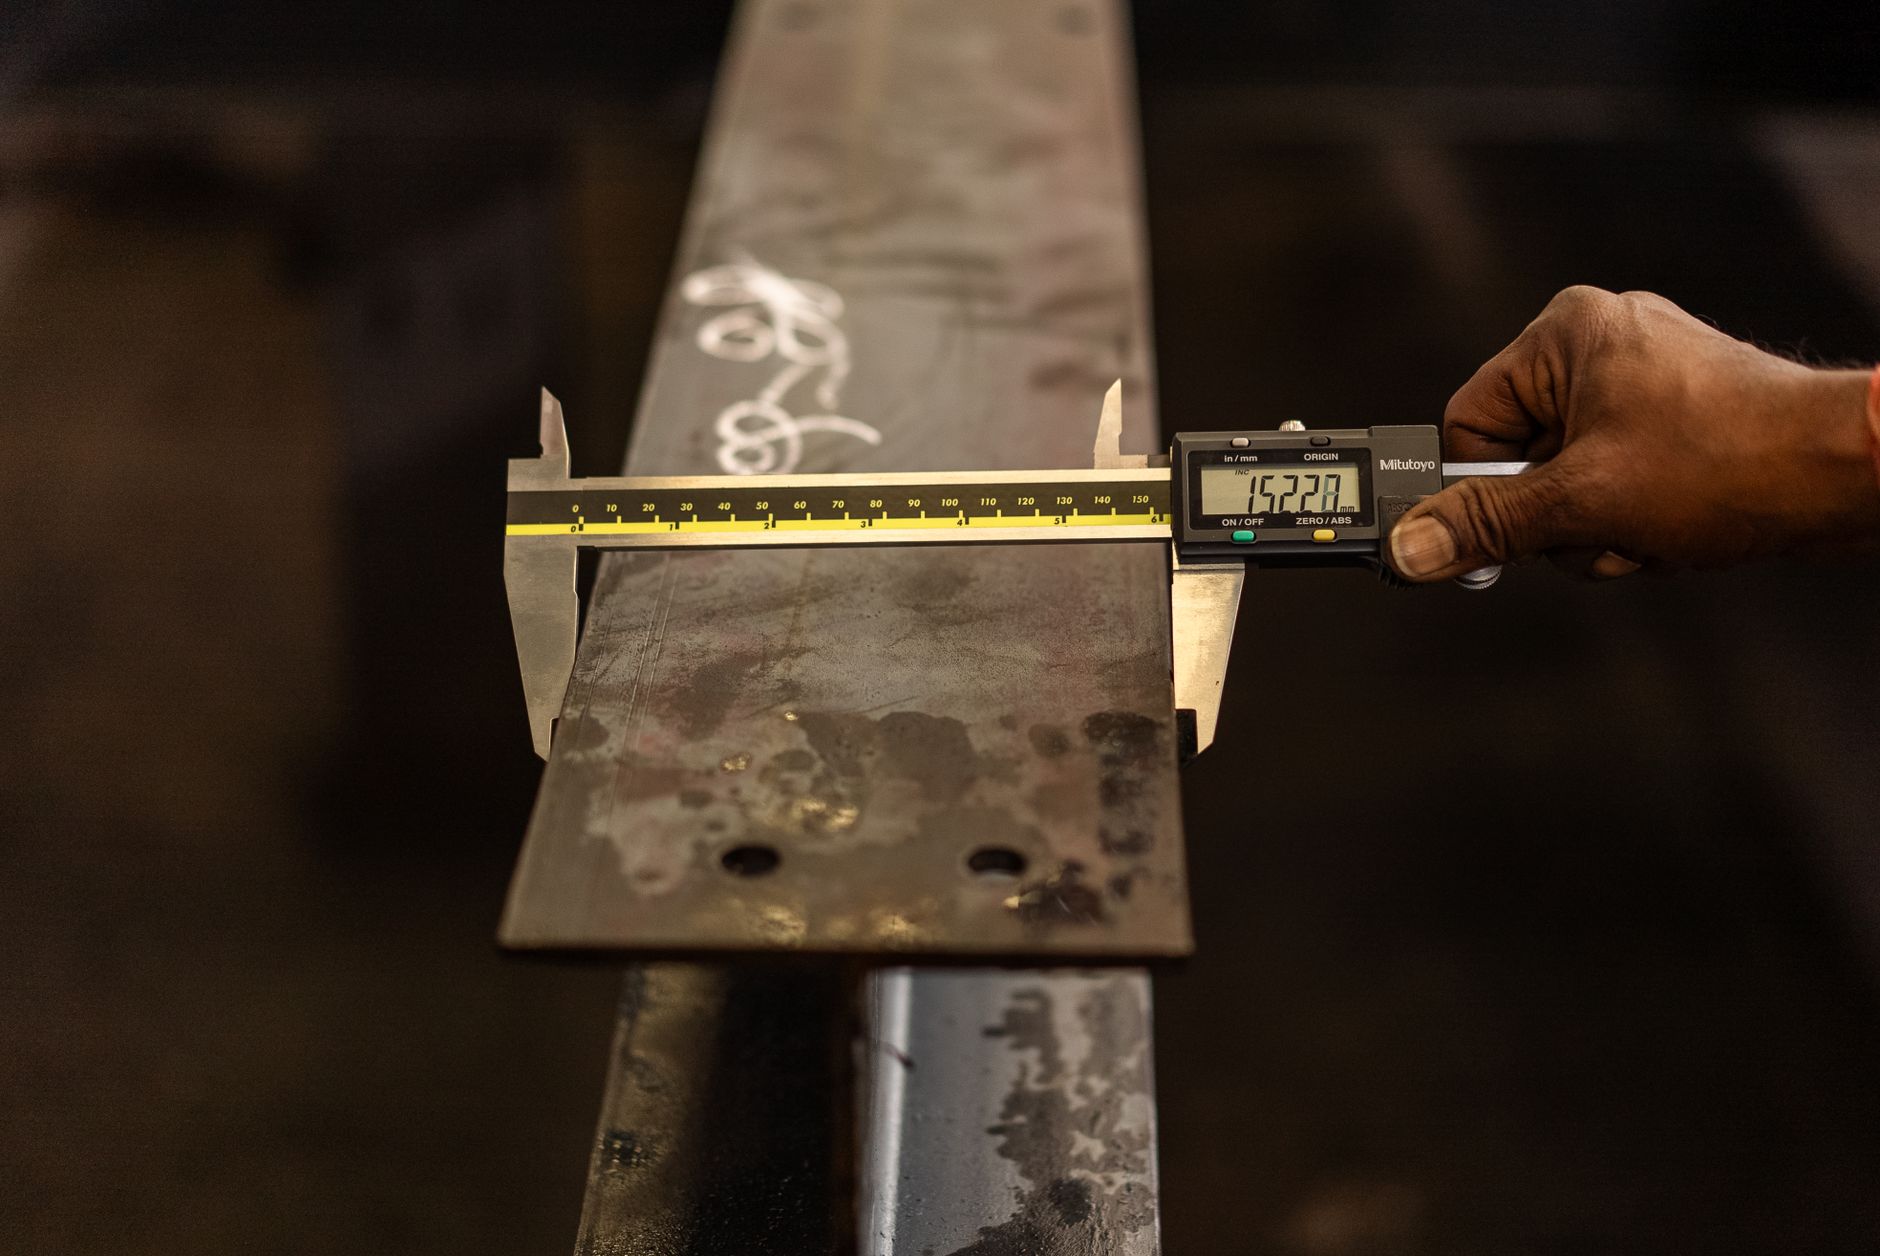
Medical devices
A five-part enclosure for a benchtop analyser, moulded in flame-rated ABS in our Class 8 bay. Every shot is weighed, and each set ships with a certificate of conformance; tolerances on the optical mounts are held to ±0.03 mm and verified on the CMM.
Automotive
Glass-filled PA66 connector housings for a Tier-1 wiring supplier, run with brass inserts overmoulded in a vertical cell. Full PPAP, IATF-controlled, with SPC on the critical pin-lead dimension and traceability from resin lot to despatch note.
From the buyers
Aster Automotive Systems
“The tool came in on the date they quoted, and the T1 report matched the drawing line for line. Two years in, the process hasn't drifted — we've stopped incoming-inspecting the part.”
Delta Instruments (M)
“Keystone took our enclosure from a rough STEP file to a validated five-cavity tool without us flying anyone over. The DFM notes alone saved us a mould revision.”
Lumen Electrical
“They run our closures to a VMI bin at our filling hall and we have never held the line for stock. Documentation for the audit was ready the same afternoon we asked.”
Before you send an RFQ
For a single-face tool of moderate complexity, six to eight weeks from a frozen design to T1 samples. Multi-cavity, hot-runner or family tools run eight to twelve. We give you a firm date with the tooling quote and a weekly build report against it.
Have a part to quote?
A quote covers the tool, the part price at your volume, the lead time and the DFM changes we'd recommend. No obligation, and your files stay under NDA.